Pressure Testing Safety: Hydrostatic & Pneumatic Safe Work Procedures

Pressure testing of piping systems, pressure vessels, boilers, and industrial pipelines is a high-consequence commissioning and maintenance activity. Stored pneumatic and hydrostatic energy, if released catastrophically due to material rupture or gasket failure, can produce violent blast waves and lethal shrapnel.
Direct Safety Takeaway: Under ASME B31.3 and OSHA regulations, hydrostatic testing (using water) is always the preferred method because liquid is virtually incompressible and stores minimal explosive energy. Pneumatic testing (using compressed air/nitrogen) stores massive compressible kinetic energy and must only be conducted under strict engineering controls with certified pressure relief valves and barricaded exclusion zones.
Hydrostatic vs. Pneumatic Testing: Risk Comparison
| Testing Method | Test Medium | Stored Kinetic Energy | Catastrophic Failure Mechanism | Required Safety Protocols |
|---|---|---|---|---|
| Hydrostatic Testing | Water or non-toxic liquid (incompressible). | Low — Pressure drops almost instantly upon structural breach. | Water jet injection, local component crack, localized flooding. | Vent all air pockets at high points before pressurization; wear eye/face protection. |
| Pneumatic Testing | Air, Nitrogen, or inert gas (highly compressible). | EXTREMELY HIGH — Behaves like an unconfined explosion. | Violent fragment projection (missile effect), supersonic shockwave. | Calculate formal blast exclusion zone; step-wise pressure increases; remote monitoring gauges. |
The 5 Core Safety Rules for Pressure Testing Operations
- 1. Calculate & Enforce Blast Exclusion Zones: Establish physical red-tape barricades around the entire test perimeter based on stored energy calculations (TNT equivalent). Only authorized test personnel are permitted within the zone.
- 2. Vent All Air During Hydrostatic Fill: Air trapped inside a hydrostatic system compresses into a hazardous pneumatic pocket. Open all high-point bleeder valves until a continuous, bubble-free water stream emerges.
- 3. Deploy Calibrated Pressure Relief Devices (PRDs): Install certified relief valves set at no higher than 110% of the maximum test pressure on all pumping manifolds.
- 4. Use Whip Checks & Hose Restraints: Secure all high-pressure flexible hoses with steel whip-check cables or hose socks at every union coupling to prevent lethal whipping if a connection fails. (See Tool Safety).
- 5. Apply Incremental Pressure Stepping: Gradually increase pressure in stages (e.g., 25%, 50%, 75%, and 100% of test pressure), holding for 10 minutes at each plateau to check for gauge stabilization. Never approach joints for visual leak checks while pressure is actively increasing.
5-Minute Safety Talk / Toolbox Topic: Stored Energy Hazards
- Meeting Question: “Why is pneumatic testing considered exponentially more dangerous than hydrostatic testing?” (Answer: Compressed gas stores massive kinetic expansion energy that acts like an explosion upon rupture).
- Perimeter Check: “Verify that our exclusion zone warning signs (‘DANGER: High Pressure Testing in Progress — Keep Out’) are posted at all entry corridors.”
- Supervisor Note: “Never tighten bolts, flanges, or fittings while a system is under pressure. Bleed pressure to 0 PSI before attempting any mechanical adjustment.”
Pre-Pressurization Safety Inspection Checklist
- ☐ Written Pressure Test Procedure and Permit approved by Lead Engineer.
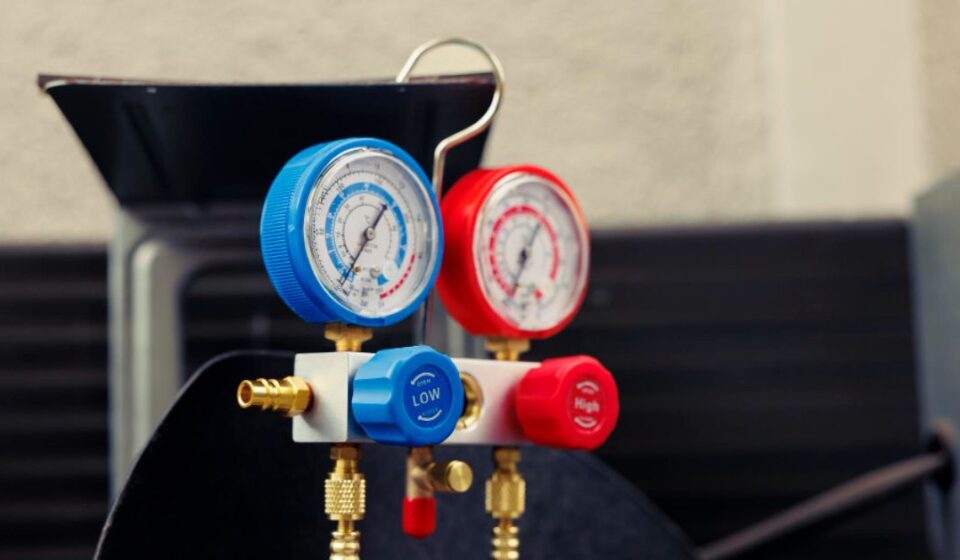
- ☐ Pressure gauges calibrated within the past 12 months with range 1.5× to 4× test pressure.
- ☐ Certified Pressure Safety Valve (PSV) installed and tested on the pump manifold.
- ☐ Whip checks installed at all high-pressure hose connections.
- ☐ High-point air bleeders checked — 100% of trapped air vented from hydrostatic system.
- ☐ Barricades and warning signage erected around calculated exclusion perimeter.
- ☐ Emergency pressure bleed-off valve accessible from outside the immediate line of fire.
Frequently Asked Questions
Can regular tap water be used for stainless steel hydrostatic testing?
For austenitic stainless steels, tap water containing chlorides can cause stress corrosion cracking. Test water must meet strict low-chloride specifications (typically < 50 ppm chlorides) and be completely drained and dried immediately post-test.
Authoritative Sources & Standards
- ASME B31.3: Process Piping — Chapter VI Inspection, Examination, and Testing.
- OSHA 29 CFR 1910.169: Air Receivers and Pressure Systems.
- API 510 / 570: Pressure Vessel and Piping Inspection Codes.